
FMEA vs PFMEA: A Complete Guide
One authoritative guide to failure mode and effects analysis — definitions, scoring, a worked example, and where monitoring data fits in.
TL;DR: FMEA (Failure Mode and Effects Analysis) is a structured method for identifying how a product or process could fail, how severe each failure would be, and how likely it is to be caught before it causes harm. PFMEA is FMEA applied specifically to a manufacturing process rather than a product design. Teams use both to rank risks by Risk Priority Number (RPN) and prioritize corrective action.
Key Takeaways
- FMEA vs PFMEA: FMEA identifies how a product design could fail; PFMEA applies the same analysis to how the manufacturing process could fail to build it correctly.
- Scoring: Every failure mode is scored on Severity, Occurrence, and Detection (1–10 each), multiplied into a Risk Priority Number (RPN) from 1 to 1,000.
- RPN is a guide, not a verdict: RPN should prioritize, not decide alone — a high-severity failure mode can warrant action regardless of its overall score.
- Data quality decides accuracy: Occurrence and Detection scores are only as good as the data behind them; ongoing monitoring turns estimates into verified numbers.
FMEA vs PFMEA at a Glance
| FMEA (Design / General) | PFMEA (Process) | |
|---|---|---|
| Focus | How the product design could fail | How the manufacturing process could produce a failure |
| Typical failure modes | Wrong material, weak tolerance stack-up, design overload | Wrong torque applied, missed operation, contamination during handling |
| Owned by | Design / product engineering | Process / manufacturing engineering |
| Created when | During product design, before tooling | Before or during process design, ahead of production launch |
| Typical output | Design changes, tolerance revisions | Process controls, fixtures, inspection points, Poka Yoke devices |
In practice, the two are sequential, not competing. A Design FMEA identifies what could go wrong with the product itself; a Process FMEA then asks how the manufacturing process might fail to build that design correctly. Most manufacturers running both treat PFMEA as the document that turns design risk into shop-floor controls.
Severity, Occurrence, Detection and the RPN Formula
Both FMEA and PFMEA score every failure mode on three scales, typically 1–10, then multiply them into a single Risk Priority Number.
| Factor | What It Measures | 1 = Low | 10 = High |
|---|---|---|---|
| Severity (S) | How serious the effect of the failure is | No noticeable effect | Safety hazard or regulatory failure |
| Occurrence (O) | How likely the failure is to happen | Extremely rare, no known history | Failure is almost certain, recurring history |
| Detection (D) | How likely current controls are to catch it before it escapes | Controls will almost certainly catch it | No control exists to catch it |
Risk Priority Number: RPN = Severity × Occurrence × Detection, giving a score from 1 to 1,000. Teams typically address the highest-RPN failure modes first, but severity thresholds often override RPN — a high-severity, low-frequency failure can still demand immediate action regardless of its overall score.
Worked Example: PFMEA for a Torque-Critical Assembly Step
Carried through a single manufacturing process step, from initial risk to closed corrective action:
| Process Step | Failure Mode | S | O | D | RPN | Corrective Action |
|---|---|---|---|---|---|---|
| Bolt torque, bracket assembly | Bolt under-torqued | 8 | 5 | 6 | 240 | Add torque wrench with auto-log and lockout below spec |
| Bolt torque, bracket assembly | Bolt over-torqued (stripped thread) | 6 | 3 | 5 | 90 | Set torque wrench upper limit alarm |
| After fix: bolt under-torqued | Bolt under-torqued | 8 | 2 | 2 | 32 | Verified via 30-day monitoring data |
Note how Occurrence and Detection both drop sharply after the corrective action — not because the team assumed the fix worked, but because thirty days of logged torque data confirmed it. That’s the difference between a PFMEA that gets filed away and one that stays accurate.
“RPN is a prioritization tool, not a decision rule. I’ve seen teams close out a failure mode because the number dropped, when nothing about the actual occurrence rate had changed — they just re-scored their own optimism.”
— Process Engineering Manager, automotive supplier
From Design FMEA to Monitored Process
A practical FMEA-to-PFMEA workflow moves through four stages:
- Design FMEA — identify how the product could fail based on its design and materials.
- Process FMEA — identify how the manufacturing process could fail to produce that design correctly, and score each failure mode.
- Corrective action — implement process controls, fixtures, or Poka Yoke devices against the highest-priority failure modes.
- Monitoring — confirm with real data that occurrence actually dropped and detection actually improved, then re-score.
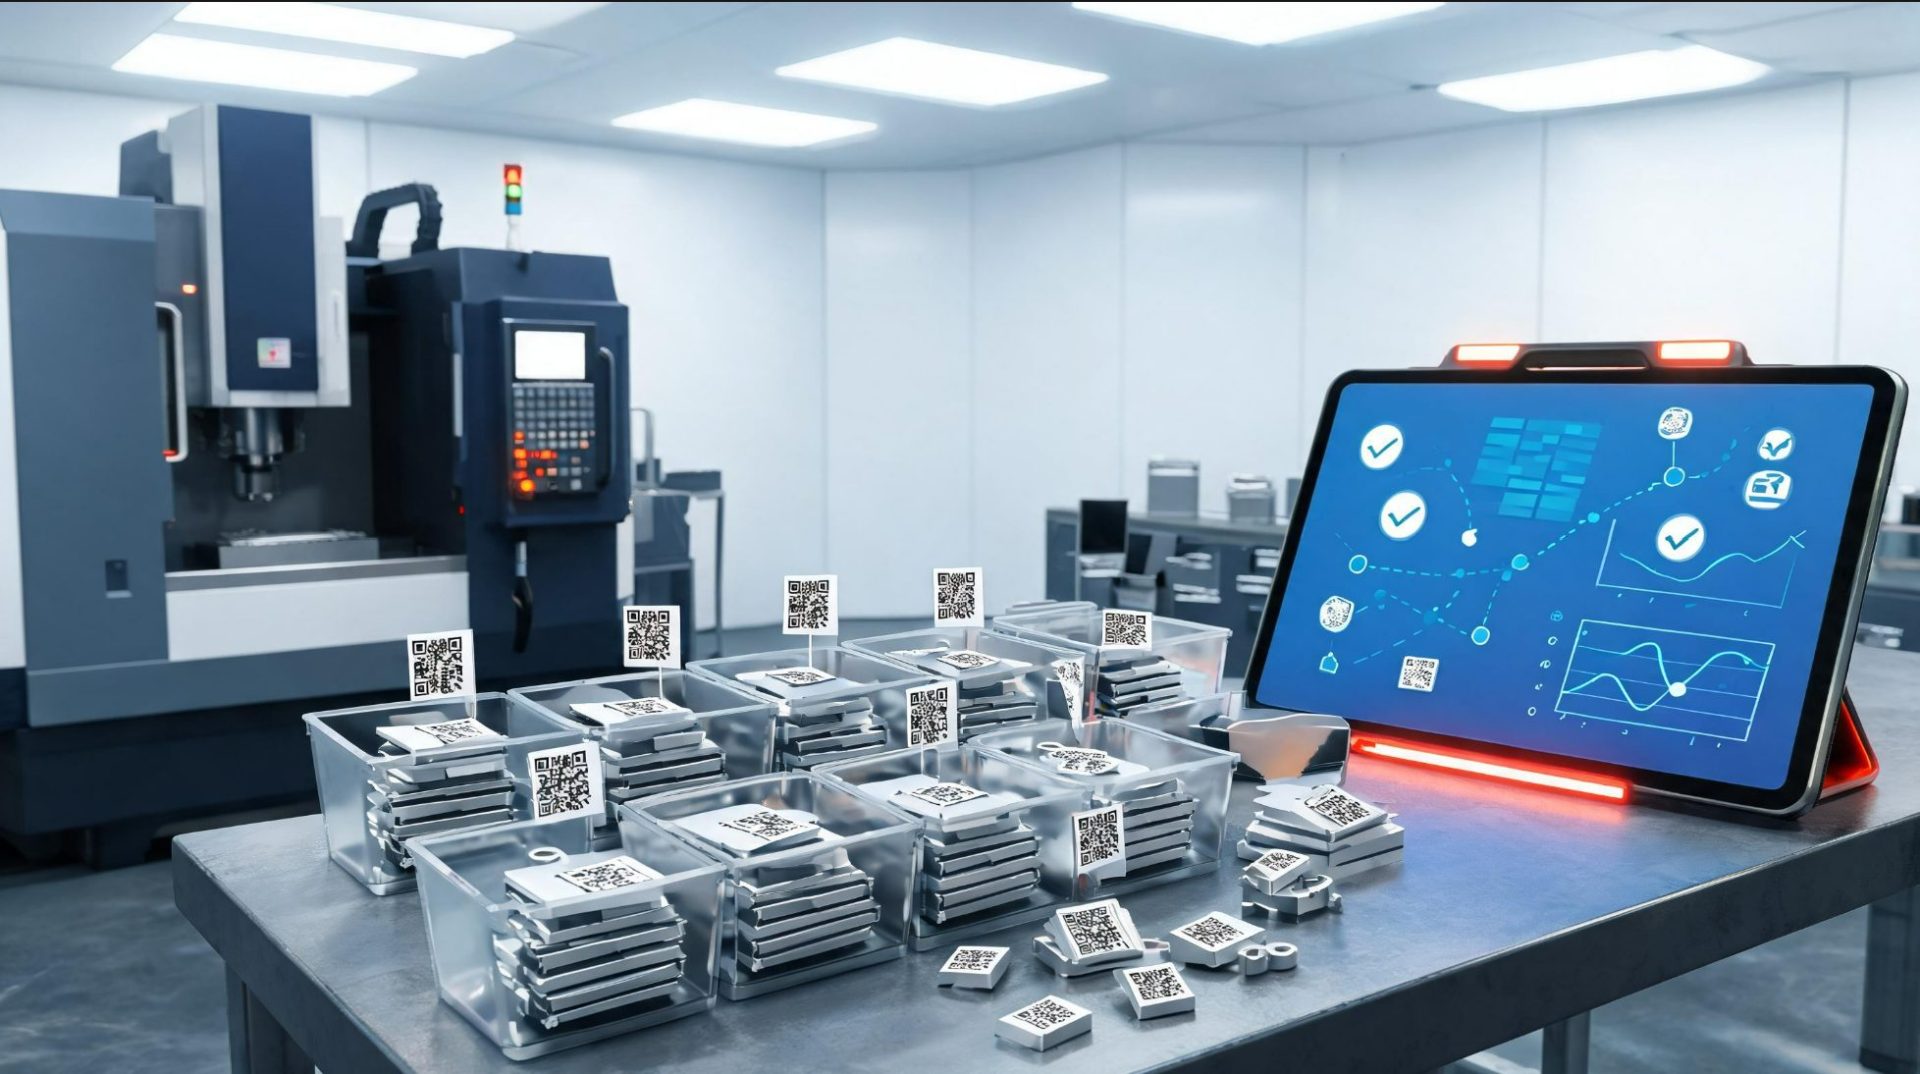
That last stage is where most PFMEAs quietly go stale. Occurrence and Detection scores are usually estimated by the team in a conference room and rarely revisited. Continuous machine and quality monitoring — the kind sfHawk provides on the shop floor — turns those estimates into measured values: actual defect frequency per failure mode, and actual time-to-detection when something does go wrong. That data either confirms the corrective action worked or flags that the PFMEA needs to be reopened.
Frequently Asked Questions
What is the difference between FMEA and PFMEA?
FMEA is the general term for Failure Mode and Effects Analysis and is often used for design-level risk. PFMEA applies the same method specifically to a manufacturing process, examining how each process step could fail to produce a conforming part rather than how the product design itself could fail.
What is a good RPN?
There is no universal “good” RPN threshold — it depends on the industry, product, and internal risk tolerance. Most teams set an action threshold (commonly in the 100–125 range) above which a failure mode requires a corrective action plan, but a high-severity failure mode should be addressed regardless of its overall RPN score.
Does FMEA follow a recognized standard?
Yes. Automotive manufacturers commonly follow the AIAG-VDA FMEA Handbook, and quality management standards such as IATF 16949 require FMEA as part of advanced product quality planning (APQP). Other industries reference FMEA guidance under ISO 9001 or sector-specific quality frameworks.
Related Reading
PFMEA is most effective when paired with the shop-floor data that validates it. See how statistical process control tracks drift in real time, and how Poka Yoke devices turn a PFMEA’s corrective actions into physical, verifiable controls.
Get Started Today! Book a call with sfHawk | Email: inquiry@sfhawk.com | Phone: +91 91120 98351 | Website: www.sfhawk.com